

A small business quality control system should make good work easier to repeat, not bury employees under forms. The goal is simple: define what acceptable work looks like, prevent predictable errors, detect important problems before the customer does, record enough evidence to learn, and improve the process when something goes wrong.
This guide shows you how to build that system from the ground up. It works for companies that make physical products, deliver professional services, prepare food, manage projects, repair equipment, fulfill online orders, or coordinate work through vendors. You do not need a dedicated quality department or expensive software to begin. You need a clear promise, a few well-placed controls, reliable records, and a disciplined method for correcting recurring problems.
Quick answer: Start with one product or service, translate customer expectations into measurable acceptance criteria, map the workflow, place prevention and inspection controls at the highest-risk points, record defects using consistent codes, contain failures immediately, investigate root causes, assign corrective actions, and review a small set of quality metrics every week. Expand only after the first process works.
 A useful quality system begins with a shared definition of acceptable work, not with more paperwork.
Part 1: Define Quality Before You Try to Control It
1. Choose one process for the first version
Do not attempt to control every activity in the business at once. Choose one process where mistakes are visible, expensive, frequent, or damaging to customer trust. Good starting points include order fulfillment, final product inspection, client report delivery, installation work, customer onboarding, food preparation, packaging, invoicing, or supplier receiving.
Write the process boundary in one sentence. For example: “This quality system covers the work from the moment an approved customer order reaches the warehouse until the packed order is handed to the carrier.” A consulting firm might write: “This system covers the preparation, internal review, approval, and delivery of monthly client reports.” A clear boundary prevents the project from turning into a vague campaign to “improve everything.”
Choose a process with enough activity to produce evidence. If it occurs only twice a year, you will wait too long to learn. The best pilot process happens weekly or daily, involves several handoffs, and produces an outcome the customer can evaluate. Once the pilot is stable, reuse the method in other areas.
2. Write a one-sentence quality promise
Your quality promise describes the result the customer should consistently receive. It should be specific enough to guide decisions but broad enough to survive minor process changes. “We provide excellent service” is too vague. “Every approved order ships with the correct item, quantity, address, documentation, and protective packaging by the promised dispatch date” is operational.
A service company might promise: “Every client deliverable is accurate, complete, written for the agreed audience, reviewed by a second qualified person, and delivered through the approved channel by the due date.” A repair shop might promise that the reported fault is confirmed, approved work is completed, safety checks are documented, and the customer receives a clear explanation of parts, labor, and remaining risks.
This promise becomes the filter for the entire system. If a form, inspection, meeting, or metric does not help the business keep the promise, it may be unnecessary. Quality control becomes bureaucratic when the organization records information without knowing which customer outcome the information protects.
3. Convert expectations into critical-to-quality requirements
Customers often describe quality with words such as reliable, professional, clean, accurate, safe, fast, durable, or easy. These words must be translated into observable requirements. Quality professionals often call these critical-to-quality characteristics, or CTQs. You can use the concept without adopting technical language throughout the company.
For a shipped product, CTQs might include the correct model, correct quantity, intact surface, functioning components, readable label, sealed package, and dispatch before a cutoff time. For bookkeeping work, they might include complete source records, correct account coding, reconciled balances, documented exceptions, restricted access, and delivery in the agreed format. For a cleaning service, they might include completed rooms, approved chemicals, no visible residue, locked doors, and photographic confirmation when required.
Each requirement should answer four questions:
- What exactly is being checked?
- What result is acceptable?
- How will a person verify it?
- What evidence, if any, must be retained?
Avoid subjective standards when a practical objective standard is possible. Instead of “package looks good,” state that the package has no open seam, crushed corner affecting protection, missing seal, incorrect label, or loose product movement beyond the permitted amount.
4. Separate defects by severity
Not every mistake deserves the same response. Create three or four defect levels so employees know what requires an immediate stop and what can be corrected during normal work.
- Critical defect: could create a safety, legal, security, regulatory, or severe customer harm. Work stops and the affected item or service is contained.
- Major defect: makes the product or service unusable, materially incorrect, or inconsistent with an important commitment.
- Minor defect: does not prevent normal use but fails a documented appearance, formatting, packaging, or presentation standard.
- Observation: not a defect yet, but a condition that could become one if the trend continues.
Define examples for your actual business. A wrong medication label would be critical in a regulated environment. A wrong shipping address is major because the order will not reach the intended customer. A small cosmetic mark may be minor for an industrial component but major for a premium display product. Severity must follow risk and customer requirements, not personal opinion.
5. Map the process as it really happens
Walk through the work with the people who perform it. List the actual steps, decisions, inputs, tools, handoffs, waiting periods, and rework loops. Do not map the ideal procedure from memory in a conference room. Observe at least several real examples.
Use a simple sequence:
- Trigger or customer request.
- Required information and materials.
- Preparation steps.
- Work or production steps.
- Handoffs and approvals.
- Final verification.
- Delivery or release.
- Customer feedback and exception handling.
Mark every point where an error can enter, remain hidden, become more expensive, or reach the customer. Pay special attention to retyping information, manual calculations, unclear ownership, similar-looking products, rushed approvals, temporary employees, undocumented changes, and work that depends on one person’s memory.
6. Establish a baseline before changing the process
Measure current performance for a short representative period. The baseline does not need to be perfect. Count completed units or jobs, defects, rework, customer complaints, returns, late deliveries, rejected supplier items, and time spent correcting errors. Use existing invoices, tickets, emails, return records, or inspection notes where possible.
Record the limitations of the data. Employees may have corrected errors without recording them. Customers may tolerate problems without complaining. A return may be coded as “customer changed mind” even when confusing product information contributed. The baseline is a starting estimate, not a verdict on the team.
A useful baseline statement might read: “During four weeks, the warehouse shipped 1,240 orders. Thirty-seven required internal rework, eighteen generated customer contacts, and nine were reshipped. Address errors and incorrect quantities represented most recorded failures.” This gives the project a clear target and prevents improvement claims based only on feelings.
Part 2: Put Controls Where They Prevent the Most Damage
7. Prefer prevention controls over final inspection
Final inspection is necessary in many processes, but it is usually the most expensive place to find an error. By that point, labor, materials, machine time, packaging, and scheduling capacity may already be consumed. A mature small business system places more effort on preventing defects and detecting them near the point of creation.
Prevention controls include required fields, templates, validated dropdown lists, barcode scanning, fixtures that allow only the correct orientation, standardized recipes, automatic calculations, approved supplier lists, access permissions, and checklists embedded in the workflow. A service company can prevent errors by using a structured client intake form instead of collecting requirements across scattered messages.
Ask of every common defect: “What allowed this error to be created?” and “What allowed it to move forward?” The first question produces prevention controls. The second produces detection controls. Both are more useful than simply telling employees to be more careful.
 Place verification close to the point where the work is performed so problems do not travel downstream.
8. Choose the right control points
Most processes need controls at several different stages. Do not add an inspection after every action. Select points based on risk, irreversibility, cost, and the chance that the problem will remain hidden.
- Incoming control: verifies materials, information, or supplier work before the business invests more effort.
- First-piece or first-job control: confirms setup before repeating the same work many times.
- In-process control: catches drift or mistakes while correction is still inexpensive.
- Handoff control: confirms that required information and status are clear before responsibility changes.
- Final release control: verifies the complete customer promise before delivery.
- Post-delivery control: monitors complaints, returns, service calls, and actual customer experience.
For a batch of printed labels, verify the first approved label before printing thousands. For a client project, review the outline and sample section before drafting the full report. For installation work, inspect concealed connections before walls or covers make them difficult to access.
9. Create standard work for the high-risk steps
Standard work is the current agreed method for completing a task safely and consistently. It should be detailed enough for a trained employee to follow but short enough to remain usable. A forty-page procedure that nobody opens does not control quality.
Use one-page job instructions, annotated photographs, short screen recordings, diagrams, examples of acceptable and unacceptable work, or numbered checklists. Include the purpose, required inputs, sequence, key limits, common mistakes, escalation point, and proof of completion. Put the instruction where the work occurs rather than hiding it in a distant shared drive.
Version-control important instructions. Show a title, owner, version number, approval date, and next review date. Remove outdated copies when the process changes. Employees should never have to guess which instruction is current.
The business can connect this quality work to its broader planning process by using a clear management plan that assigns ownership, resources, milestones, and review dates instead of treating quality as an isolated project.
10. Design checklists around failure points
A checklist should protect against forgetting a small number of important items. It should not restate every movement in the job. Build it from observed defects, customer requirements, safety risks, and mandatory records.
Write each check as a verifiable statement: “Customer name and shipping address match the approved order,” not “Check customer details.” Use yes/no, pass/fail, a measured value, or a required attachment. Group checks in the sequence of the work. Place stop points before irreversible actions such as payment release, final printing, shipment, installation, publication, or deletion.
Test the checklist with real employees. If every item is automatically marked without thought, it is too long, too vague, or disconnected from consequences. Remove low-value items and improve unclear ones. A good checklist creates a brief deliberate pause at the moments where human memory is most likely to fail.
11. Use risk-based sampling instead of checking everything
One hundred percent inspection is appropriate for some critical characteristics, new suppliers, unstable processes, one-off custom jobs, or items where a single failure can cause serious harm. It is wasteful and still imperfect for many routine low-risk activities. Employees become fatigued, inspections delay flow, and the process may continue producing defects because the organization relies on sorting them out later.
Use a simple risk-based sampling rule. Increase the sample when the item is new, the supplier recently changed, the process was adjusted, the defect is serious, the history is poor, or the batch is unusually large. Reduce the sample only after a stable period with reliable evidence. Return to increased inspection immediately after a failure.
For example, a business might inspect the first five units after setup, then one unit every hour, and the final unit before release. A service team might review every deliverable from a new employee, then move to selected work after demonstrated competence. Document the rule so sampling is not adjusted merely to meet a deadline.
12. Make acceptance criteria visible
Inspectors cannot make consistent decisions if the standard lives only in a manager’s head. Create an acceptance card for each important output. Include the requirement, method, tolerance or limit, defect severity, and action when the result fails.
Use photographs for visual standards. Show acceptable, borderline, and unacceptable examples under similar lighting and scale. For written or digital work, provide an approved model and a list of mandatory elements. For customer service, define required verification, tone boundaries, response commitments, and escalation conditions.
Whenever possible, replace “looks right” with a measurable or observable statement. If judgment is unavoidable, train employees using the same examples and compare their decisions. Disagreement between inspectors is a signal that the standard needs clarification or the measurement method is unreliable.
13. Verify the measurement method
A quality system can create false confidence when the tool or method is inconsistent. Check whether scales, gauges, thermometers, timers, software formulas, templates, cameras, barcode scanners, or manual counts produce reliable results.
For basic equipment, compare readings with a known reference at planned intervals and record the result. Follow manufacturer requirements and any applicable regulatory rules. Label tools that are damaged, overdue for verification, or unsuitable for precision work. Do not allow employees to keep using a questionable tool because it is the only one nearby.
For human inspection, ask two trained people to evaluate the same small sample independently. If their decisions differ often, improve the definition, lighting, sample preparation, training, or tool. The objective is not to blame the inspectors; it is to make the decision system repeatable.
14. Create a clear hold-and-release status
Employees need to know whether work is awaiting inspection, accepted, rejected, being reworked, or approved under a documented exception. Physical items can use separate zones, colored tags, labeled containers, or system status fields. Digital work can use restricted folders, workflow states, or approval permissions.
Never allow rejected work to sit beside accepted work without a visible difference. Accidental mixing is a common cause of repeat customer failures. Assign authority for release. The same person who performed the work may complete routine self-checks, but higher-risk outputs may require independent approval.
An exception or deviation should identify the specific requirement, reason, risk, authorized person, affected quantity or customer, expiration date, and any extra control. Temporary acceptance must not quietly become the new standard.
Part 3: Build Records That Help People Learn
15. Keep the inspection record minimal but useful
A small business usually needs fewer fields than it expects. Record only information that supports traceability, release, analysis, compliance, or customer protection. A practical record may include date, order or batch, product or service, process stage, checker, checks performed, result, measured value where needed, defect code, disposition, and evidence link.
Use a spreadsheet, form, project-management tool, point-of-sale record, or quality module already available to the business. Software should follow the process rather than dictate it. Begin with a simple system that employees will use correctly. Add automation after you understand which fields and reports matter.
Make required fields truly required. Use dropdown lists for recurring defect categories. Protect formulas and reference lists. Limit access to sensitive customer or employee information. Create a backup and retention routine consistent with the importance and legal requirements of the records.
16. Create a small defect-code library
Free-text descriptions make analysis difficult because the same issue is recorded as “wrong item,” “incorrect SKU,” “picking error,” and “customer received different product.” Create ten to twenty codes for the most meaningful defect types. Use a hierarchy only if volume justifies it.
For an order operation, codes might include wrong item, wrong quantity, damaged before packing, damaged packaging, address error, missing document, late dispatch, supplier defect, system data error, and customer specification unclear. For professional services, codes might include incomplete requirements, factual error, calculation error, formatting nonconformance, missed review, privacy concern, late delivery, and unauthorized scope change.
Keep an “other” code, but review it monthly. If many records use it, create a better category. Do not create so many codes that employees cannot choose. The purpose is to reveal patterns, not to describe every event with perfect precision.
17. Preserve traceability proportional to risk
Traceability means being able to connect an output to the information needed to investigate it. Depending on the business, that may include supplier lot, production batch, machine, employee, work order, software version, source file, approval, date, location, or customer requirements.
Do not collect identifiers with no practical use. Ask what information would be needed if a customer reports a defect, a supplier announces a problem, or a regulator requests evidence. High-risk and regulated products may require formal lot control and retention rules. A low-risk service company may need only project version history, reviewers, and approval records.
Test traceability by selecting a finished item or delivered project and attempting to reconstruct its path. Then start with a supplier lot or source file and identify all affected outputs. If this takes days or depends on one person’s memory, improve the system before a real incident occurs.
18. Record rework separately from a clean pass
If an employee finds and fixes a defect before delivery, the customer may receive acceptable work, but the process did not perform correctly the first time. Record the failure and the rework. Otherwise, the dashboard will show perfect quality while labor and capacity are being consumed by hidden correction.
Use result options such as pass first time, pass after rework, rejected, scrapped, returned to supplier, customer concession, or canceled. Track approximate rework time when practical. The objective is not to punish employees for finding problems. Early detection is valuable. The objective is to see where the process creates avoidable work.
Managers should praise honest reporting and improvement. If defect data is used primarily to embarrass individuals, employees will hide errors, change codes, or avoid documenting borderline conditions. A quality system depends on psychological and operational permission to surface problems.
19. Control documents and templates
Quality failures often come from an outdated price list, drawing, recipe, contract clause, client brief, specification, or spreadsheet. Store controlled documents in one approved location. Restrict editing rights, show version and effective date, and define who approves changes.
When a document changes, identify affected people, active jobs, inventory, suppliers, customers, and training. Withdraw obsolete versions. For an emergency change, record the decision and complete formal review afterward. Do not let “temporary” files circulate indefinitely through email attachments.
Use descriptive filenames and avoid versions such as final, final2, and final-revised. A consistent pattern might include document name, process, version, and approval date. For cloud tools, use built-in version history and permissions rather than creating uncontrolled copies.
 Quality records should connect the finished result to the process, version, people, and materials that produced it.
Part 4: Respond to Defects Without Repeating Them
20. Contain the problem before investigating it
When a serious defect is found, first protect customers and prevent additional exposure. Stop the affected process if necessary. Identify and separate suspect work. Check inventory, active jobs, recent deliveries, and related batches. Preserve evidence before changing settings or reworking everything.
Containment is a temporary protective action, not the final solution. Examples include increased inspection, holding shipments, disabling an incorrect template, notifying affected employees, using an approved alternative supplier, or contacting customers who may have received the problem.
Assign one incident owner. Record what is known, what is uncertain, affected scope, immediate decisions, and next review time. Avoid public speculation and blame. If the issue may involve safety, law, regulation, cybersecurity, or significant financial harm, use the appropriate professional and authority promptly.
21. Decide the disposition of nonconforming work
Every rejected item or deliverable needs a controlled outcome. Common dispositions include rework to the original requirement, repair under an approved method, return to supplier, scrap, redo, reclassify for a different legitimate use, accept with authorized customer concession, or cancel.
Define who may approve each option. A production employee should not independently decide that a failed safety requirement is “close enough.” Rework instructions must be clear, and the corrected work should be re-inspected. If rework can introduce a new problem, add the relevant verification.
Record the quantity, reason, approval, cost where useful, and final status. Make sure scrapped or rejected items cannot reenter normal stock. For digital work, prevent an obsolete file from being delivered after correction by controlling access and naming.
22. Investigate the process, not only the person
Human error is a description, not a root cause. Ask why the error was likely or possible. Was the instruction unclear? Were two products visually similar? Did the software permit an invalid selection? Was workload unrealistic? Did the employee lack training or practice? Was information missing? Did a manager approve a shortcut? Was the control removed to meet a deadline?
Use the “five whys” carefully. Begin with a specific event and continue until the team identifies a controllable system condition. Do not force exactly five questions. Stop when evidence supports the cause and the proposed action can prevent recurrence.
For complex failures, group possible causes under people, method, equipment, material or information, environment, and measurement. Verify causes with records, observation, tests, and interviews. A plausible story is not enough. If replacing a worn fixture eliminates the defect under controlled conditions, the evidence is stronger than an assumption that employees became careless.
 Root-cause work should turn a specific failure into a testable explanation and a practical process change.
23. Separate correction from corrective action
A correction fixes the current problem. Corrective action changes the system to reduce the chance of recurrence. Replacing the wrong item in a customer’s order is a correction. Adding barcode verification, separating similar items, and updating the picking screen may be corrective actions.
Record both. Otherwise, the business may provide excellent customer recovery while paying for the same failure repeatedly. Conversely, do not launch a large corrective-action project for every isolated minor defect. Use thresholds based on severity, frequency, trend, customer impact, and cost.
A corrective action should have an owner, due date, planned change, required resources, risk review, training or document updates, and a method for checking effectiveness. Avoid vague actions such as “remind staff” unless the cause was genuinely a one-time communication failure and the reminder can be verified.
24. Verify effectiveness after implementation
Closing an action because a new form was created does not prove the problem is solved. Decide in advance what evidence will demonstrate effectiveness. This might be zero recurrence across a defined number of jobs, a reduced defect rate, successful audit observations, improved supplier results, or consistent use of the new control.
Allow enough time and volume for a meaningful test. Review unintended consequences. A new double-check may reduce errors but create late deliveries or cause employees to bypass the system during busy periods. Improve the control if it is too difficult to sustain.
If the defect recurs, reopen the investigation. The original cause may have been wrong, the action may have been incomplete, or another pathway may create the same symptom. Treat recurrence as new evidence rather than a reason to repeat the same instruction more forcefully.
25. Communicate with customers factually
When a customer is affected, acknowledge the issue, explain the verified facts, state the immediate protection or correction, provide a realistic next step, and identify a contact person. Do not speculate, minimize the impact, blame a supplier, or promise an outcome you cannot deliver.
Use plain language. A concise message might say: “We identified that your shipment may contain the incorrect adapter. Please do not use the affected item. We have arranged a replacement and return label, and our team is checking all orders prepared during the same period. We will update you by 3 p.m. tomorrow.”
Train employees on which incidents they may resolve and which require management, legal, security, insurance, or regulatory review. The site’s guide on writing clear business emails can help teams communicate actions, deadlines, and evidence without using vague or defensive language.
Part 5: Extend Quality Beyond the Inspection Table
26. Assign quality responsibilities across the business
Quality is not owned only by the person who performs final checks. Leadership defines priorities and resources. Process owners maintain standards. Employees follow and improve the method. Inspectors verify results. Purchasing manages supplier requirements. Sales confirms promises are realistic. Customer service captures feedback. Someone coordinates data and corrective actions.
Create a simple responsibility table for the pilot process. For each major activity, identify who performs it, who approves it, who provides information, and who must be informed. Keep accountability with one named role rather than a committee.
Protect the authority to stop or hold work when a critical requirement fails. Employees should not need to choose between meeting a shipment target and preventing known defective work from reaching a customer. Leadership behavior determines whether the written quality policy has meaning.
27. Train for competence, not attendance
A signed training sheet proves that information was presented, not that the employee can perform the work. Define the required competence for each controlled task. Use explanation, demonstration, supervised practice, observation, and a realistic test.
For a visual inspection, the employee should correctly classify known samples. For a service process, the employee should complete a simulated case using the current template and escalation rules. For equipment, the employee should demonstrate setup, normal operation, checks, shutdown, and response to abnormal conditions.
Record the task, trainer, date, evidence, result, restrictions, and review or retraining trigger. Retrain after major changes, repeated errors, long absence, or evidence that the method is not understood. Pair quality training with the company’s broader employee onboarding and role-development process rather than treating it as a one-time orientation document.
28. Make self-inspection safe and honest
Small teams often cannot assign a separate inspector to every task. Self-inspection can work when acceptance criteria are clear, evidence is retained, serious decisions receive independent review, and employees are not rewarded for hiding problems.
Build a short pause between doing and checking. Change perspective: review the work against the original requirement, use a checklist, compare with a reference, or inspect in a different sequence. For written work, review factual accuracy separately from style. For order packing, scan the item after it enters the package rather than relying on the pick action alone.
Use periodic layered checks by a supervisor or peer to verify that self-inspection remains effective. The purpose is not surveillance. It is to detect drift, unclear standards, and conditions employees may no longer notice because they see them every day.
29. Build supplier quality into purchasing
A company cannot inspect quality into unreliable materials indefinitely. Define supplier requirements before ordering: specification, approved samples, labeling, packaging, documentation, traceability, delivery conditions, change notification, defect handling, and response time.
Classify suppliers by risk. A supplier providing a safety-critical component, confidential data service, or single-source item deserves more qualification and monitoring than a replaceable low-cost office supply. Review capability, references, certifications where relevant, sample performance, communication, and business continuity.
Track supplier defects consistently. Share evidence and request containment and corrective action for serious or recurring failures. Do not shift specifications informally through phone calls. Use controlled purchase requirements and approve changes. Reduce receiving inspection only after stable performance and restore it when evidence changes.
30. Adapt the system for service businesses
Service quality is often harder to see because production and consumption may happen together. Control the inputs, decisions, handoffs, communication, and records that shape the customer experience.
A service quality plan may include complete intake information, confirmed scope, qualified assignment, response time, approved method, review of high-risk work, privacy controls, documented customer approval, and closure confirmation. Use call recordings only where lawful and appropriately disclosed. Protect personal and confidential information.
Measure first-time resolution, reopened cases, missed commitments, correction time, incomplete intake, customer effort, and complaint themes. Avoid treating satisfaction scores as the only evidence. A friendly interaction can still produce an incorrect result, while a technically correct outcome can fail because the customer was not informed.
31. Use customer feedback as quality data
Combine formal complaints with returns, refunds, repeated questions, support contacts, lost customers, reviews, warranty claims, canceled orders, and sales objections. A complaint is not merely a customer-service event; it is evidence about the process.
Code feedback using the same defect categories where possible. Record product, service, date, channel, severity, verified cause, resolution, and whether similar cases exist. Avoid counting one incident multiple times when it generates an email, refund, return, and replacement.
Close the loop with the process owner. A monthly slide showing complaint totals is not enough. Assign investigation and action where thresholds are reached. Also look for positive feedback that identifies which process features customers value and should be protected during improvement.
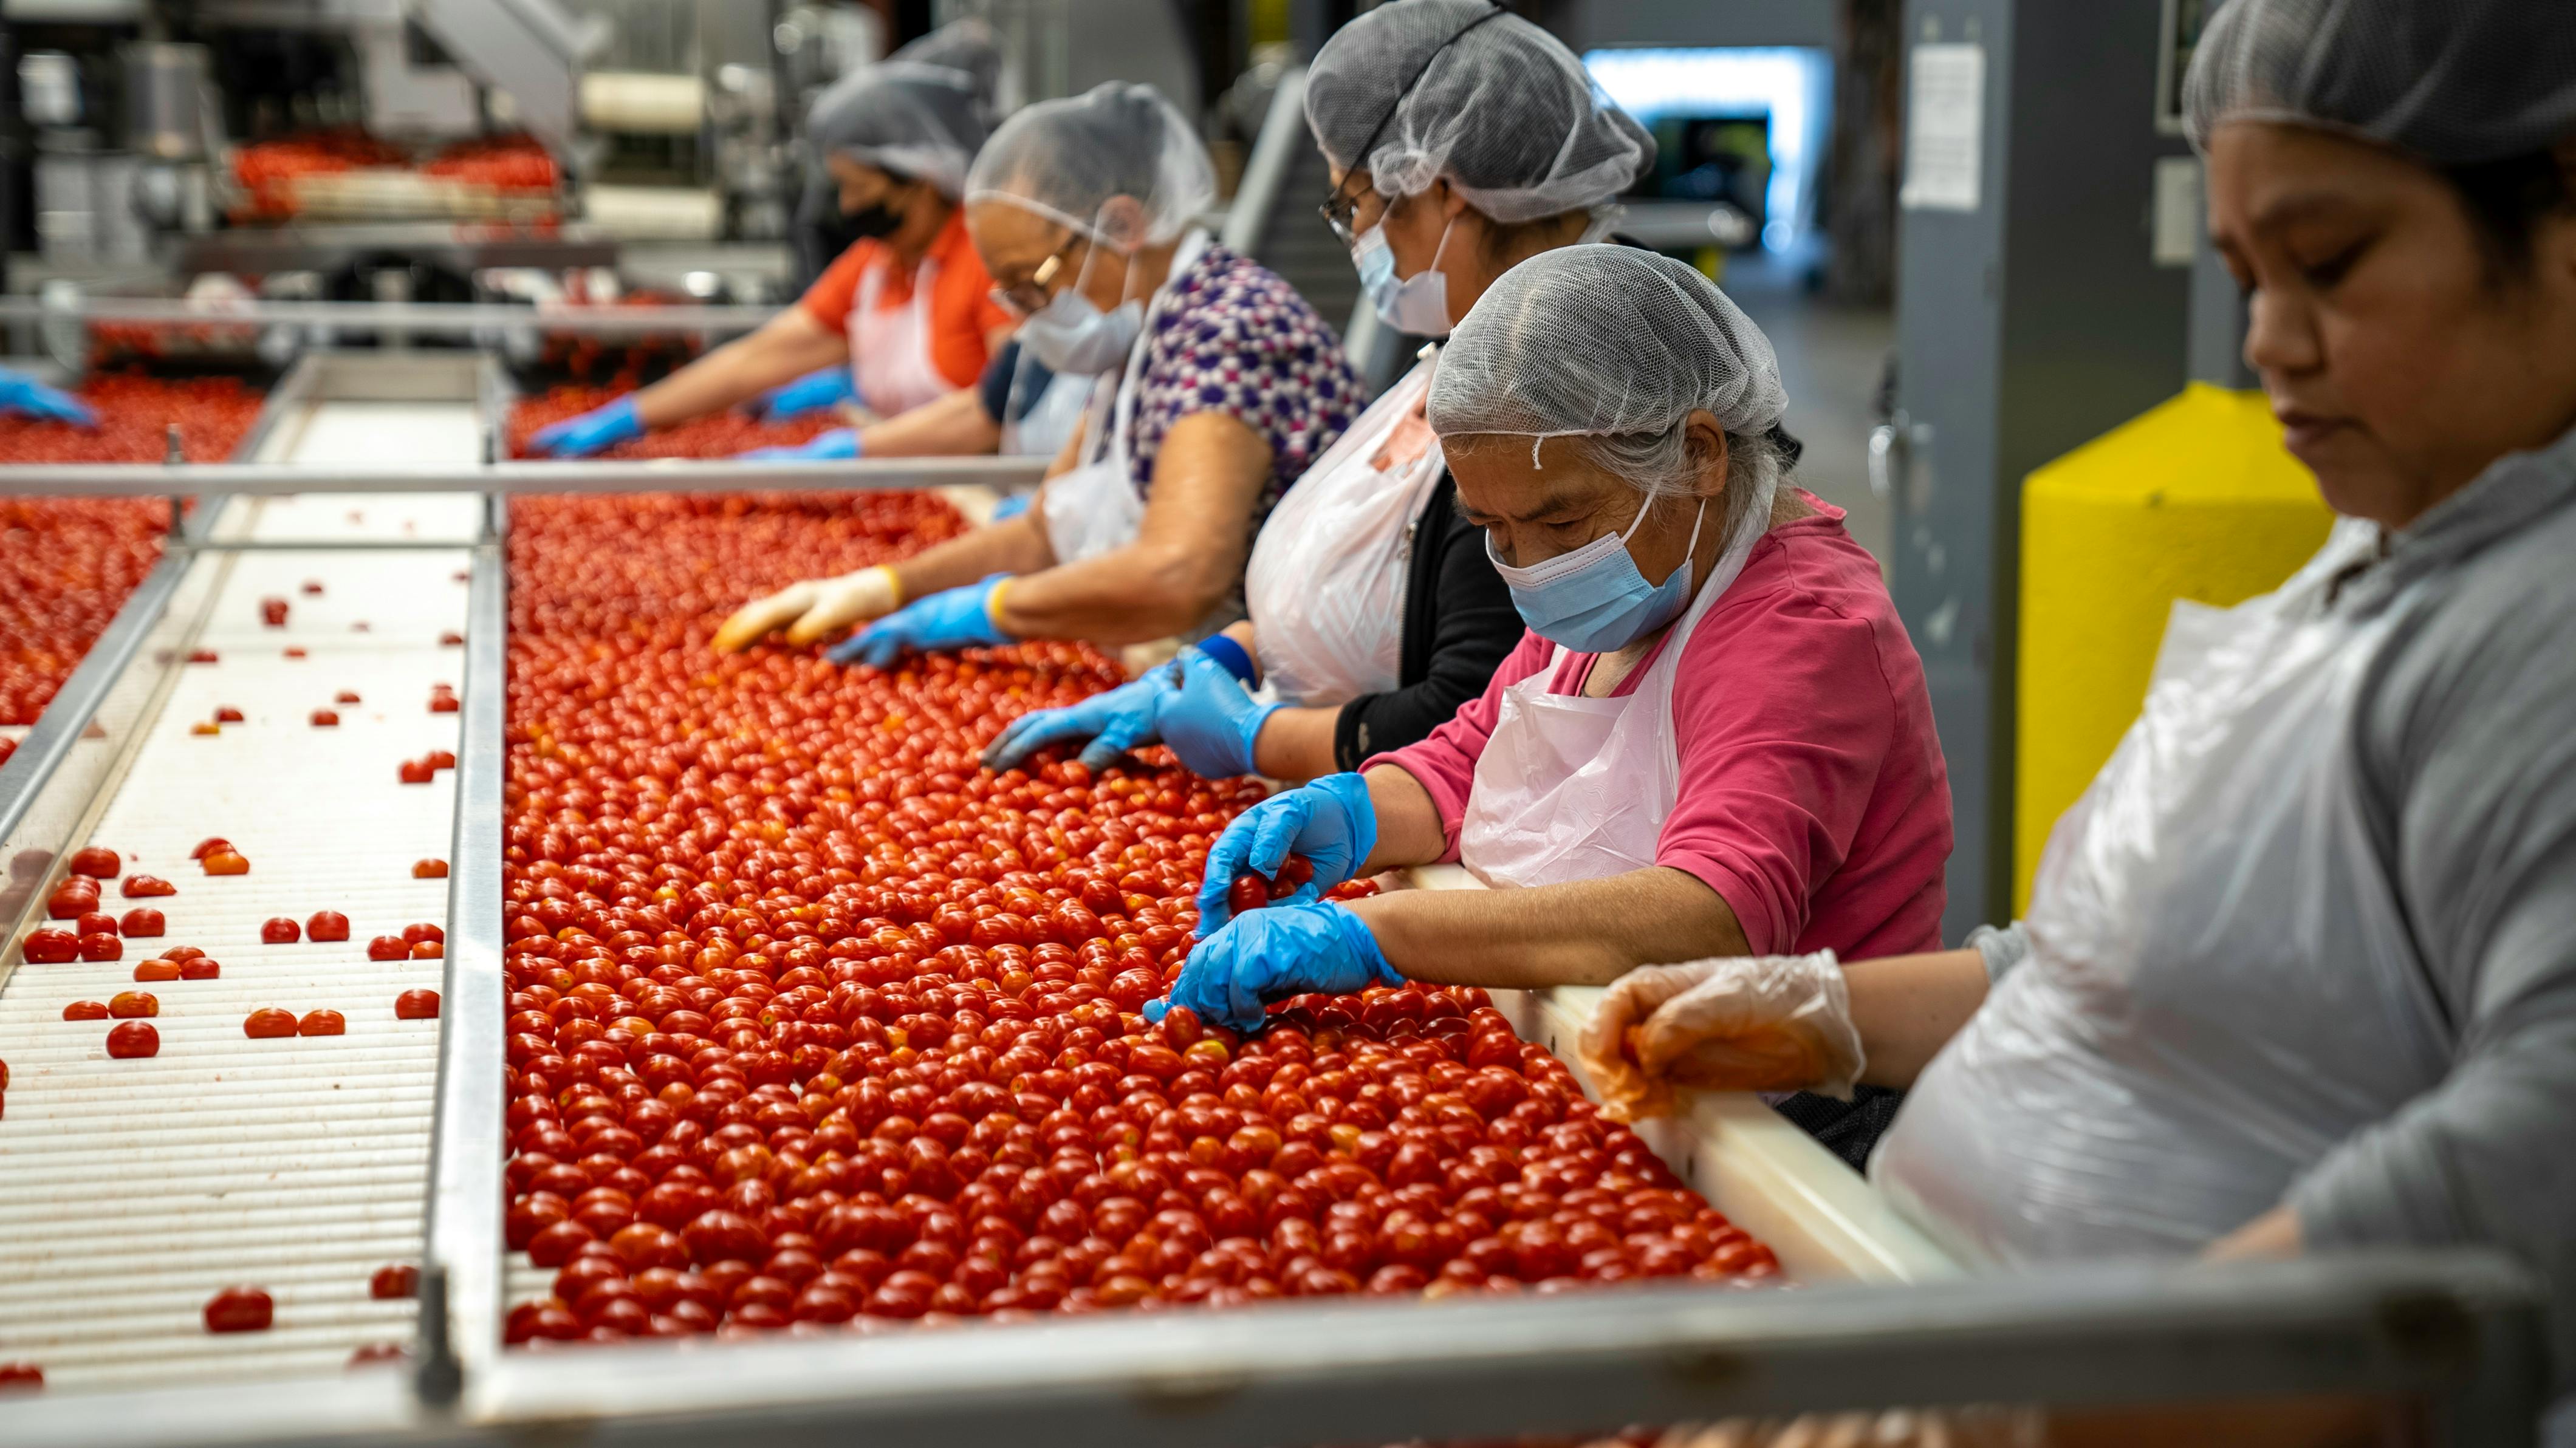 Consistent quality comes from clear standards, trained people, suitable conditions, and rapid removal of nonconforming output.
Part 6: Measure What Helps You Improve
32. Track first-pass yield
First-pass yield is the percentage of units or jobs that meet requirements without rework. Divide the number that pass the first time by the total completed, then multiply by 100. If 470 of 500 orders pass without correction, first-pass yield is 94 percent.
This metric exposes hidden work that final-pass quality misses. A team can deliver every order correctly after correction while spending hours fixing preventable errors. Track first-pass yield for the whole process and, where useful, at high-risk stages.
Define what counts as rework before reporting. Do not change the definition to improve the number. Pair the rate with volume and defect severity. A high percentage may still be unacceptable if the small number of failures is critical.
33. Measure defect and complaint rates using a denominator
Raw defect counts can mislead when business volume changes. Calculate defects per hundred units, per thousand orders, per service case, per labor hour, or another meaningful denominator. Keep the denominator consistent long enough to see a trend.
Separate internal defects from customer escapes. Internal detection is less damaging than a customer finding the problem, but both reveal process performance. Track severity and type. Ten minor formatting errors do not necessarily carry the same risk as one critical privacy failure.
Review counts and rates together. A falling rate with rapidly growing volume may still increase the total workload of correction. A rising rate in a low-volume product may be hidden in company-wide averages.
34. Estimate the cost of poor quality
The cost of poor quality includes rework labor, scrap, replacement materials, express shipping, refunds, credits, warranty work, complaint handling, repeated inspections, supplier returns, downtime, lost capacity, and preventable customer loss. Begin with costs you can estimate reliably.
For each significant defect category, calculate approximate occurrences multiplied by average correction cost. Add direct costs and note major indirect effects separately. The objective is not accounting precision; it is prioritization. A frequent small error may consume more money than a dramatic but rare problem.
Also track prevention and appraisal costs when making investment decisions. A modest fixture, software validation, or supplier improvement may reduce much larger failure costs. Present the business case in terms leadership can compare with other priorities.
35. Monitor process signals, not only final outcomes
Final defects are lagging indicators. Add a few leading indicators that show whether the process is under control. Examples include overdue training, expired tool verification, missing first-piece approval, open corrective actions, supplier change notices, incomplete specifications, checklist completion, or backlog beyond a safe limit.
Choose signals with a demonstrated relationship to quality. Do not create a dashboard of everything the software can count. Each metric should have an owner, definition, source, target or trigger, review frequency, and expected action.
Use simple charts over time. A weekly or monthly trend is more informative than a single red or green status. Investigate sudden shifts, repeated spikes, and gradual deterioration. Do not react to normal random variation with constant process changes.
36. Review a one-page quality dashboard
A small business dashboard can fit on one page. Include volume, first-pass yield, internal defect rate, customer escape or complaint rate, top three defect types, rework time or cost, supplier defects, overdue corrective actions, and one brief improvement update.
Review it weekly during the pilot and monthly after stability. Focus the meeting on decisions: which problem needs investigation, what action is blocked, whether a control is working, and what risk has changed. Do not spend the meeting reading numbers that participants could review in advance.
Record decisions, owners, and due dates. Close actions visibly. A dashboard without follow-through becomes decorative reporting and teaches employees that quality data has no practical consequence.
37. Conduct short process audits
A process audit checks whether the current method is understood, available, followed, and effective. It is not a surprise search for someone to blame. Select a small sample of work and observe the process, records, equipment, status controls, and employee understanding.
Ask employees to explain the requirement, show the current instruction, demonstrate the check, and describe what they do when the result fails. Compare actual work with the documented method. If the real method is better and safe, update the document. If an essential control is routinely bypassed, investigate why.
Record findings as conforming practice, improvement opportunity, minor nonconformance, or serious nonconformance according to defined rules. Assign actions based on risk. Verify closure instead of treating the audit report as the endpoint.
38. Use management review to remove systemic barriers
At planned intervals, leadership should review customer feedback, process performance, supplier results, audit findings, corrective actions, resource needs, changes, risks, and improvement opportunities. This resembles the evidence-based, process-focused approach described in the ISO quality management principles.
The meeting should answer whether the system is suitable, used, effective, and adequately resourced. Leadership may need to approve equipment, staffing, supplier changes, software improvements, training time, or revised commitments to customers.
Certification to ISO 9001 is not required to benefit from quality-management principles. Companies with customer, industry, or regulatory requirements can explore formal support through resources such as the NIST Manufacturing Extension Partnership quality-management services. A lightweight internal system should not be described as certified unless an accredited certification process has actually been completed.
Part 7: Launch the System in 30 Days
Days 1–5: Define scope, promise, and baseline
Select the pilot process, appoint an owner, and write the boundary. Interview employees and at least a small number of customers or customer-facing staff. Create the quality promise and list the critical requirements. Classify defect severity. Collect recent defect, rework, complaint, return, and delivery evidence.
Walk the process from start to finish. Photograph or note handoffs and decision points. Identify the three most expensive or risky failures. Do not start writing procedures for every task. The first week should produce a clear problem statement and a baseline.
Completion test: the team can explain which process is included, what the customer must receive, which failures matter most, and how current performance will be measured.
Days 6–10: Build standards and control points
Create acceptance cards for the critical requirements. Develop visual examples where relevant. Select incoming, first-job, in-process, handoff, and final checks based on risk. Decide which characteristics require every-unit verification and which can use sampling.
Draft short standard-work instructions for the highest-risk steps. Design a practical checklist and test it on real work. Establish accepted, held, rejected, and rework status. Verify that measuring tools and software calculations are suitable.
Completion test: two trained people can evaluate the same work and reach substantially the same result, and failed work cannot accidentally move forward without a visible decision.
Days 11–15: Create records and defect handling
Build the inspection form, defect codes, nonconformance log, and disposition choices. Define required traceability and document control. Write the immediate containment procedure and assign authority for release, rework, scrap, supplier return, and customer communication.
Create a simple corrective-action form with problem, containment, evidence, root cause, action, owner, due date, and effectiveness review. Test the entire record flow with one historical defect. Remove fields that nobody can explain or use.
Completion test: a recorded defect can be traced from discovery through containment, decision, correction, analysis, and closure without relying on private messages or memory.
Days 16–20: Train and run a controlled pilot
Train employees on the customer promise, critical requirements, checks, defect severity, stop authority, records, and escalation. Use actual examples and supervised practice. Verify competence rather than collecting attendance signatures only.
Run the system on a limited number of orders, jobs, or batches. Keep the process owner available to answer questions. Record every point of confusion. Do not punish employees for finding more defects during the pilot; improved visibility is an expected result.
Completion test: employees can perform checks, classify common defects, isolate failed work, find the correct instruction, and explain whom to contact for an abnormal situation.
Days 21–25: Analyze data and fix the first recurring problem
Calculate first-pass yield, defect rates, rework, complaints, and the most common defect categories. Choose one recurring meaningful problem. Contain it, investigate the process, implement a proportionate corrective action, and set an effectiveness check.
Review supplier involvement, workload, information quality, equipment, layout, software, and training. Avoid automatically selecting an employee reminder. Make the change observable and testable.
Completion test: the team has completed at least one full learning cycle from evidence to verified process change.
Days 26–30: Simplify, assign governance, and expand carefully
Ask employees which parts of the system prevent errors and which create effort without value. Simplify forms, remove duplicate entry, clarify definitions, and automate only stable steps. Finalize the one-page dashboard and meeting schedule.
Assign document owners, training triggers, audit frequency, supplier review, metric review, and management review. Decide whether the next priority is expanding the pilot process, applying the method to a second process, or stabilizing current controls longer.
Completion test: the system has named owners, employees use it during normal workload, quality data produces decisions, and the business can sustain it without the founder personally checking every item.
Practical Templates You Can Build Today
One-page quality standard card
- Output or service name.
- Customer or use.
- Critical requirement.
- Acceptance limit or example.
- Verification method.
- Defect severity.
- Required evidence.
- Action when failed.
- Owner, version, and approval date.
Inspection record
- Date and time.
- Order, batch, project, or case ID.
- Process stage.
- Checker.
- Checks and measured values.
- Pass first time, pass after rework, or fail.
- Defect code and severity.
- Disposition and approver.
- Evidence or attachment link.
Corrective-action record
- Specific problem statement.
- Affected scope and risk.
- Immediate containment.
- Evidence reviewed.
- Verified root cause.
- Correction for current cases.
- Corrective action to prevent recurrence.
- Owner, resources, and due date.
- Document, training, supplier, or system changes.
- Effectiveness measure and review date.
Common Mistakes That Make Quality Systems Fail
Writing procedures before observing the work
The resulting documents describe what management imagines rather than what employees can perform. Observe real work, include operators in design, and test instructions before approval.
Inspecting everything at the end
This creates delay, fatigue, and expensive rework. Move controls toward the point of error and add prevention mechanisms.
Measuring employees instead of the process
Individual accountability matters, but most recurring defects involve unclear information, poor tools, difficult layouts, uncontrolled changes, or unrealistic flow. Use evidence before assigning cause.
Using too many forms and codes
Complexity lowers data quality. Begin with the minimum information needed for control and learning. Add detail only when a decision requires it.
Closing actions when paperwork is complete
A new procedure or training session does not prove effectiveness. Review actual performance after enough time and volume.
Rewarding speed while punishing defect reporting
Employees will hide problems or bypass checks. Align targets so stopping a serious defect is recognized as protecting the business.
Confusing certification with quality
A certificate can support customer confidence and market requirements, but only daily process behavior creates consistent outcomes. Build an effective system first and pursue formal certification when there is a clear business reason.
Frequently Asked Questions
Does a very small business need a quality control system?
Yes, but it should match the company’s size and risk. A five-person business may need one-page standards, a shared defect log, clear approval rules, and a weekly review rather than a separate department. The absence of bureaucracy does not require the absence of control.
What is the difference between quality assurance and quality control?
Quality assurance focuses on designing and managing processes that are capable of producing acceptable results. Quality control focuses on verifying outputs and responding when they do not meet requirements. A practical system uses both: prevention through good process design and detection through appropriate checks.
Should every product or service be inspected?
Not necessarily. Inspect every unit or case when risk, regulation, customer requirements, instability, or severity justifies it. Use documented risk-based sampling for stable lower-risk work. Critical characteristics may still require complete verification even when other characteristics are sampled.
How many quality metrics should a small business track?
Start with five to eight: volume, first-pass yield, internal defect rate, customer complaint or escape rate, rework time or cost, top defect types, supplier defects, and overdue corrective actions. Add a metric only when someone owns it and knows what action a change should trigger.
Can spreadsheets support the first system?
Yes. A protected spreadsheet and simple form can be sufficient for a controlled pilot. Use consistent fields, permissions, backups, validation, and version control. Move to specialized software when volume, traceability, workflow complexity, regulation, or integration creates a real need.
How do we prevent quality checks from slowing delivery?
Prevent errors upstream, automate reliable validations, inspect at the source, use risk-based sampling, simplify checklists, and remove duplicate recording. Measure inspection time and delay. Never remove a critical control only to improve a speed metric; redesign the process instead.
What should happen when an employee repeatedly makes the same error?
Confirm the requirement, training, tools, workload, supervision, process design, and evidence. Retrain and observe competence where appropriate. If the system is clear and usable but an employee knowingly ignores it, use the company’s fair performance process. Do not label every recurrence as carelessness before investigating.
When should a company consider ISO 9001 certification?
Consider it when customers require it, target markets value it, supply-chain qualification depends on it, or leadership wants an independently audited management system. Certification requires a formal scope, implemented system, records, internal audits, management review, and an accredited external certification process. It should solve a business need rather than serve as a decorative badge.
Final Takeaway
A strong small business quality control system is not a stack of documents. It is a repeatable agreement about what customers must receive, where errors are most likely, how work is verified, what happens when requirements fail, and how evidence changes the process.
Begin with one important workflow. Write the quality promise, define five to ten critical requirements, place controls at the highest-risk points, and record failures consistently. The most important mistake to avoid is relying on final inspection and employee memory while the underlying process continues creating defects.
Your first practical action is to select one recent customer problem and trace it backward through the workflow. Identify where it was created, where it could have been prevented, and where it should have been detected. That single exercise will show you where the first useful quality control belongs.